The total value of membrane performance
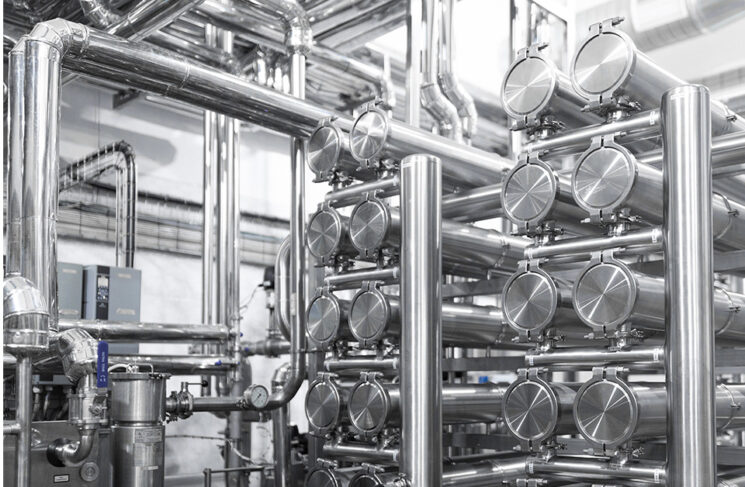
Membrane performance determines how much product you recover, how consistently you meet specification, and how efficiently your system operates. Solecta measures performance through Total Value of Operation (TVO), helping you maximize yield, reduce operating costs, and identify the right time for membrane replacement.
Recommendations built on your feed stream and your data

Understand your objectives
We start with your performance targets and the constraints your plant runs under, so every recommendation ties back to a result your team is measured on.

Evaluate the process
We review feed characteristics, operating conditions, and performance data to find the variables with the largest effect on yield.

Engineer for the application
Solecta membranes are designed around specific separations. We match membrane chemistry and element design to your process and production targets.

Validate performance
We measure membrane performance under your operating conditions and analyze the results. Those findings guide process optimization, membrane selection, and replacement timing.
Explore the Possibilities
Our team of application engineers and domain experts understands your industry’s unique challenges. (They’re also eager to solve them.)





Proven results in real-world operations
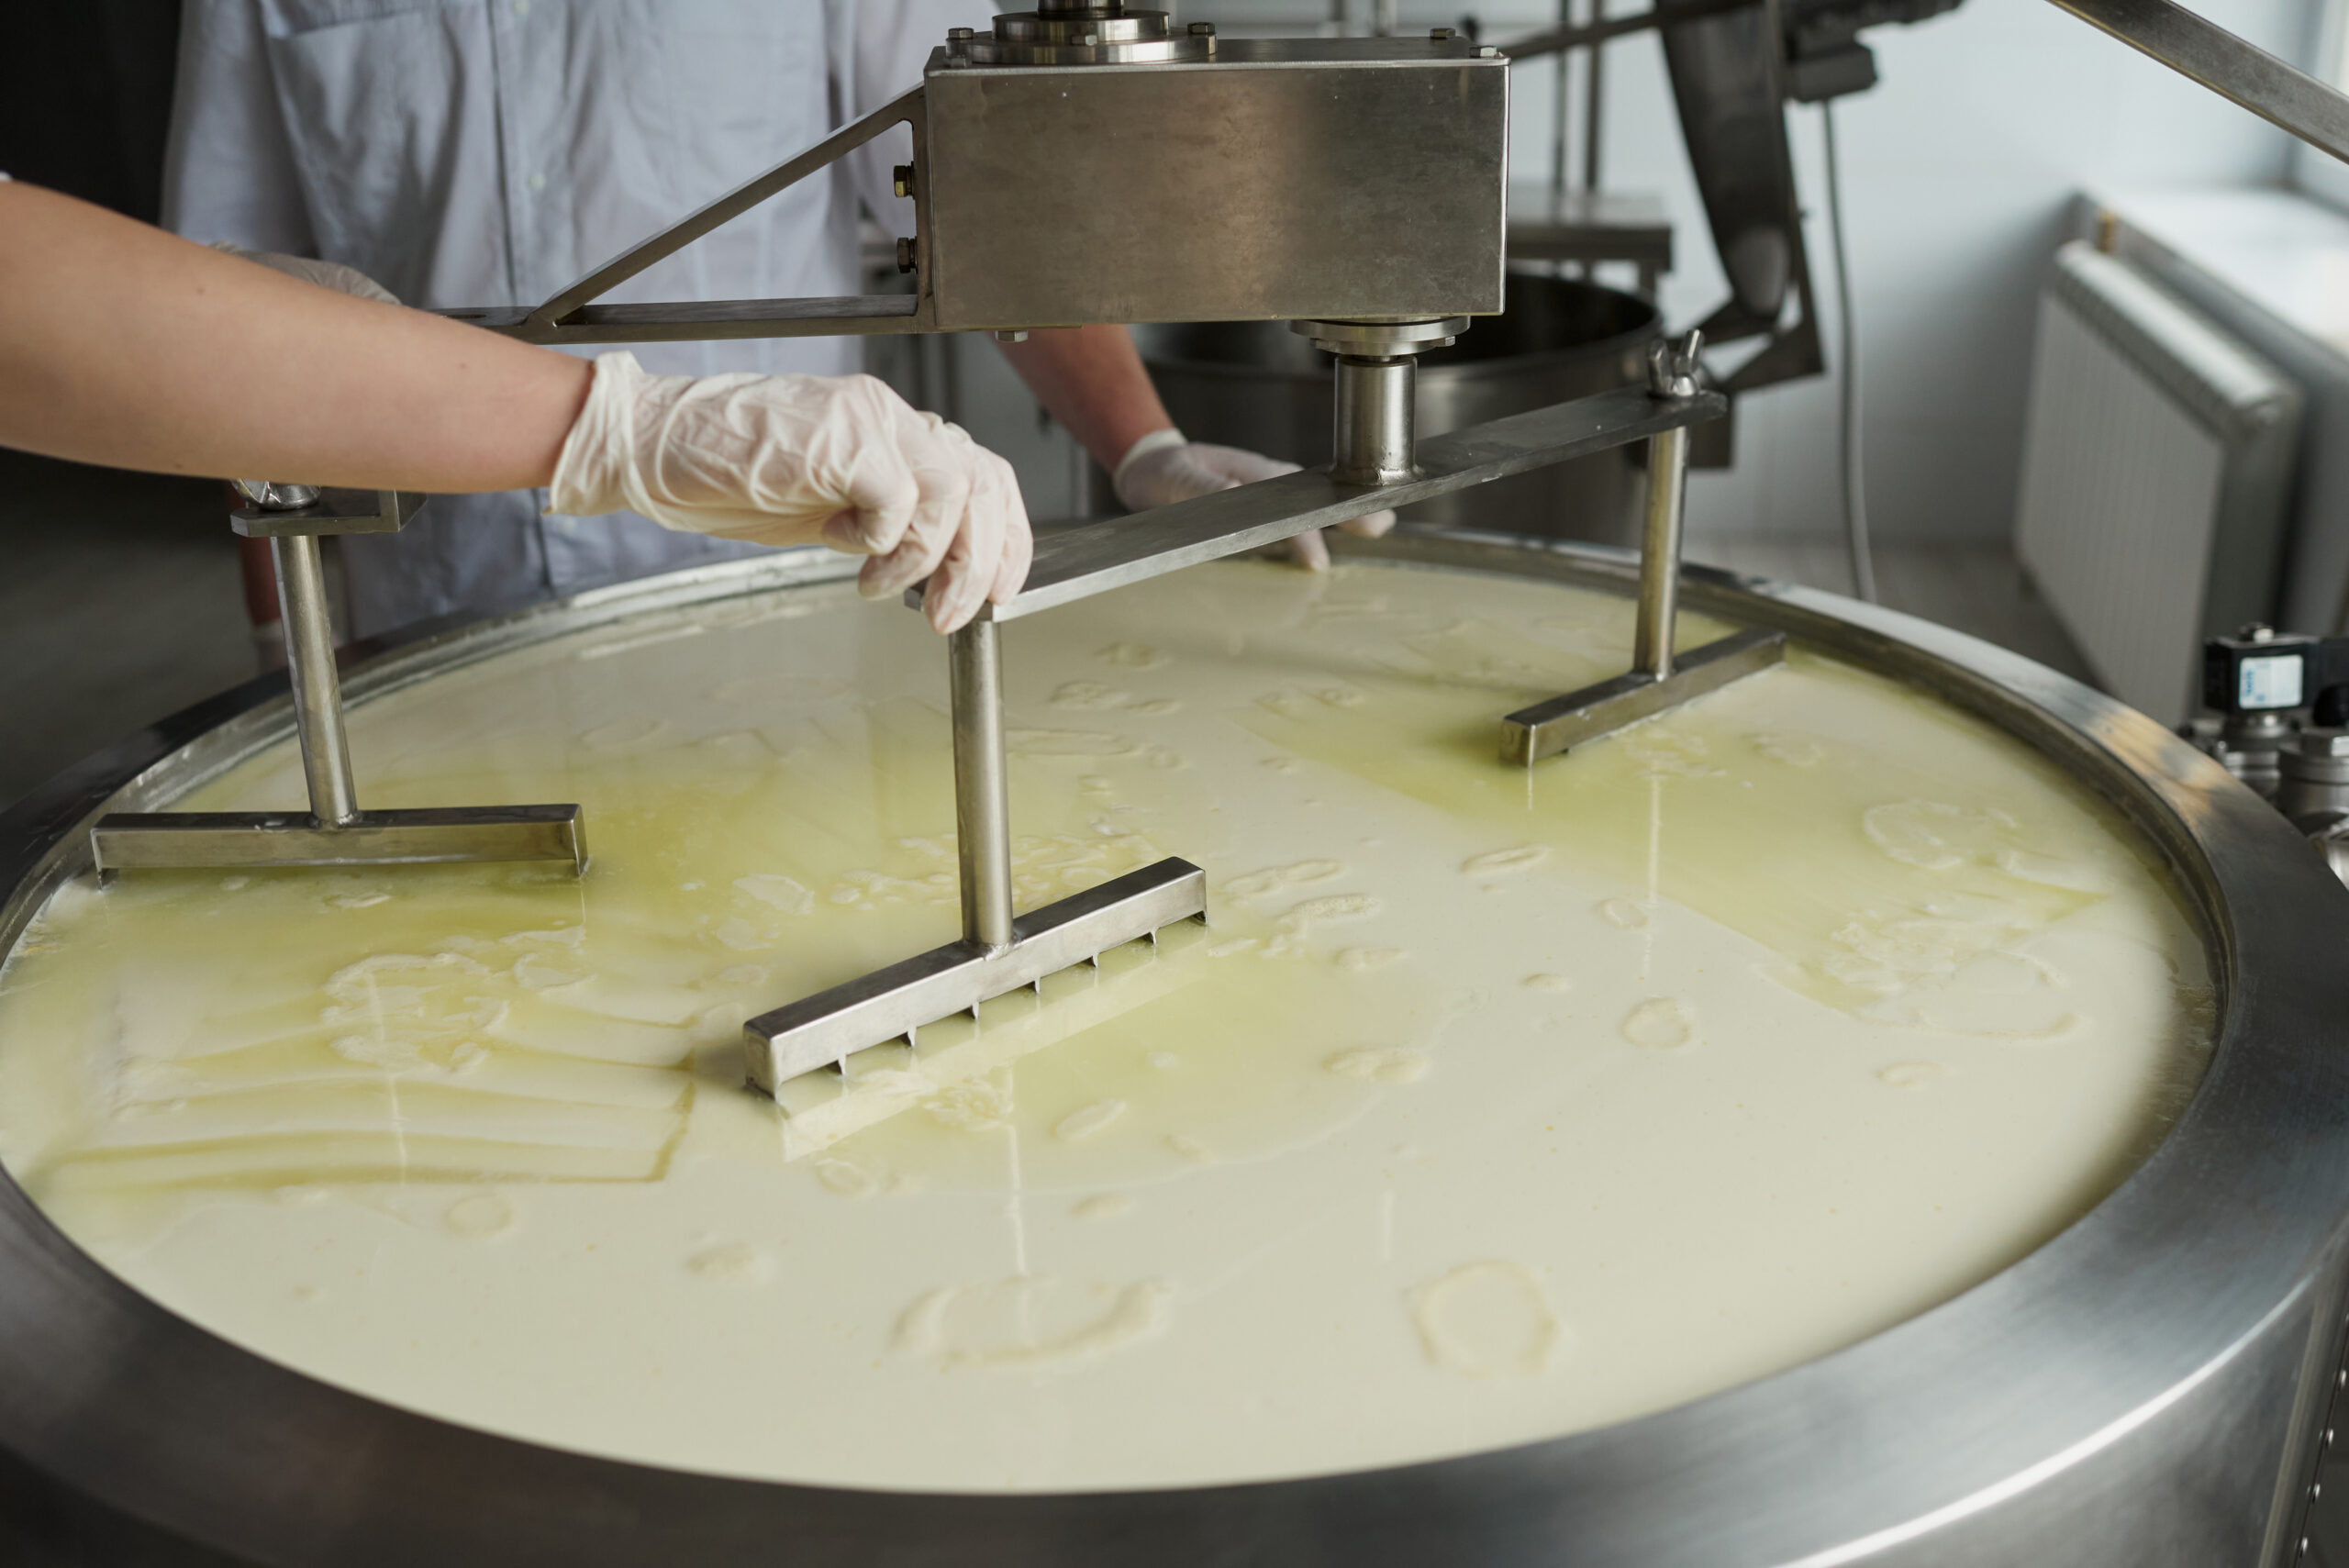
5.76% higher protein recovery
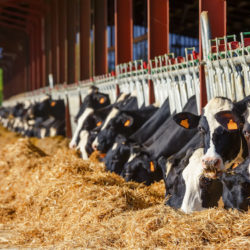
Dairy microfiltration (MF)
A Wisconsin cheese processor tested Solecta membranes on one MF train against two incumbent membrane sets running the same whey feed. Protein recovery rose from 80.52% to 85.16%, a 5.76% relative gain, and the plant then switched all three MF trains.


Bring us your separation challenge
If you are developing a new application or trying to get more from an existing membrane process, our applications engineers will work through it with your team. We start with your feed stream, product specifications, and production goals, then match the membrane to them.